
Cooling Built for Dairy's Demands
Alpine engineered a custom chiller system specifically for Gracemar Farms, ensuring consistent cooling that keeps up with dairy production and protects valuable equipment.
Alpine Refrigeration partnered with Gracemar Farms in Chilliwack, BC, to deliver a custom dairy chiller retrofit that solved chronic ammonia issues and extended equipment life.
The retrofit integrated an advanced clean-room design and heat recovery, reclaiming waste heat to provide warm water for livestock and boiler preheat - turning a 7-year-lifecycle problem into a 25-30-year asset.
The project also opened the door to Investment Agriculture Foundation (IAF) sustainability grants for the farm, delivering financial and environmental benefits alongside the technical fix.
These upgrades created a more sustainable, cost-efficient system built to last for decades.
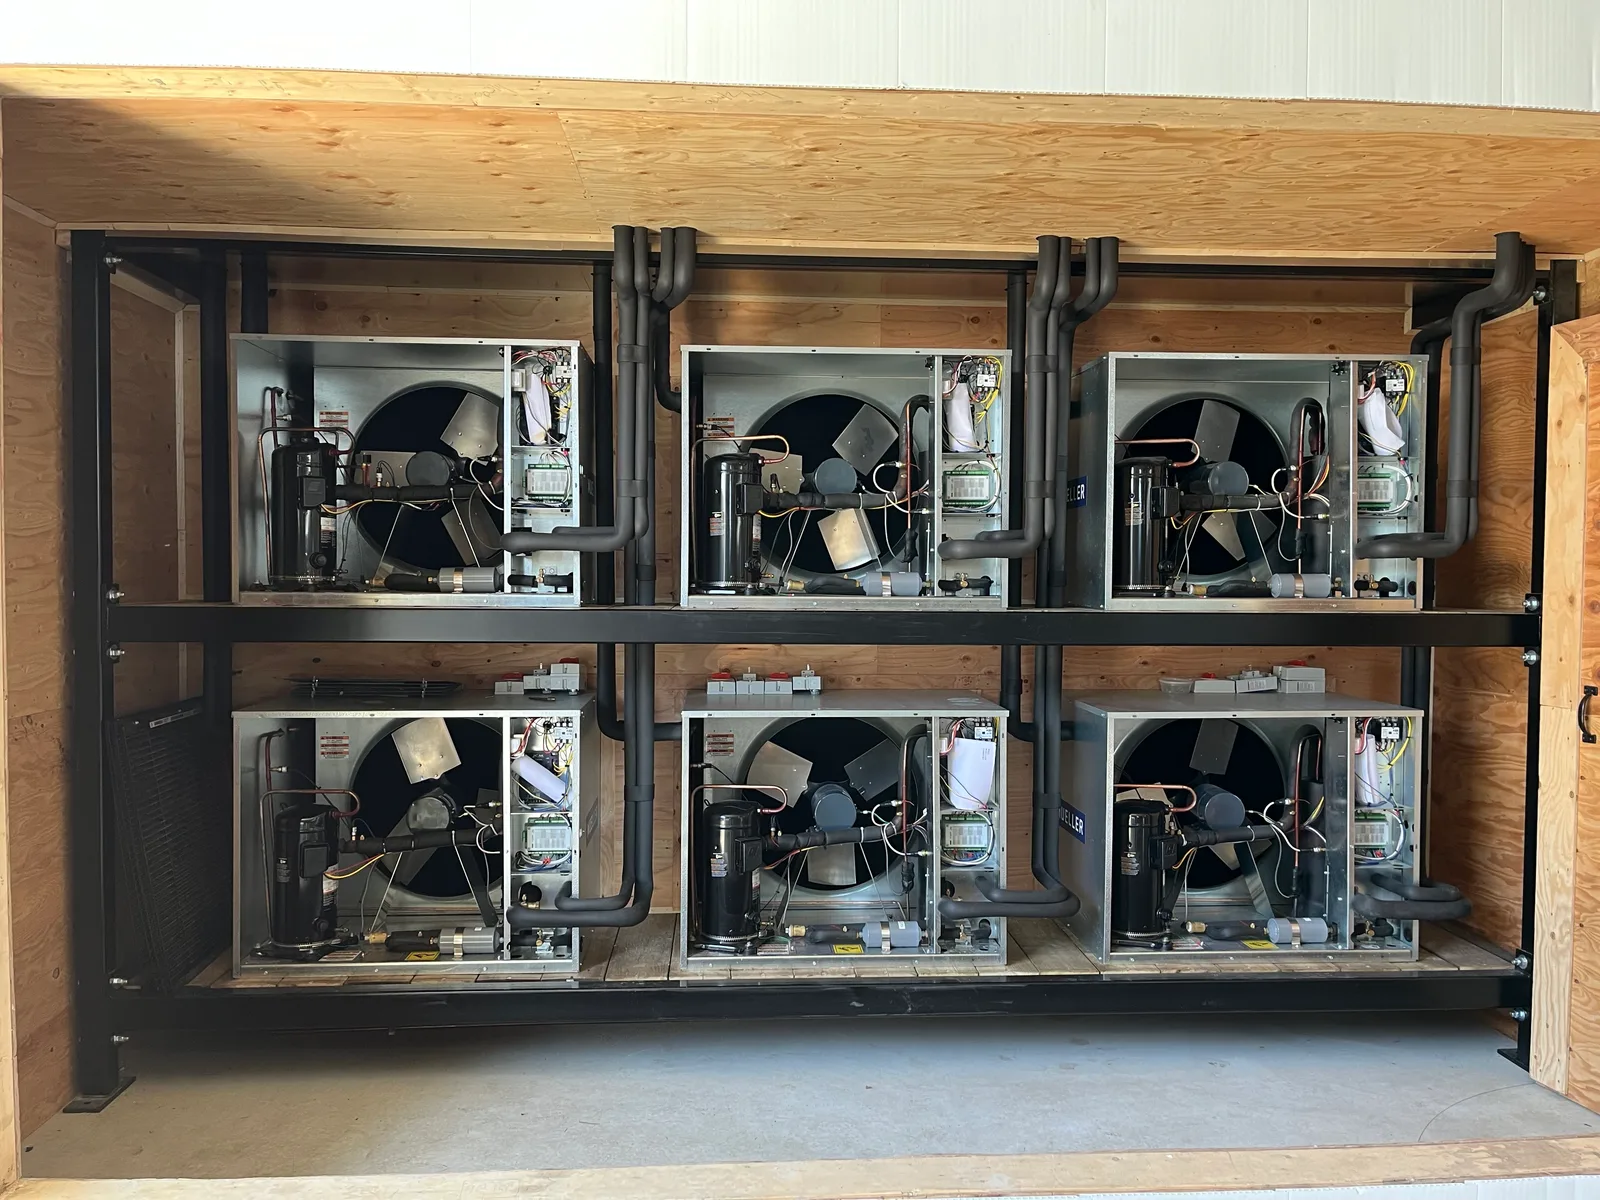
The clean-room layout and new equipment racks that replaced Gracemar's legacy plant - the old system averaged only seven years between replacements.
Gracemar Farms was operating with outdated refrigeration equipment that created chronic ammonia issues and limited system reliability. Equipment lifespans averaged only 7 years, leading to frequent replacements, high costs, and constant maintenance demands.
The existing system also wasted significant amounts of heat energy, offering no recovery process to repurpose excess thermal output. This inefficiency raised operating expenses and missed opportunities to support livestock operations more sustainably.
At the same time, regulatory pressures around air quality and environmental compliance meant a long-term solution was needed - one that would improve safety, extend system life, and support sustainable farming practices.

Custom piping and control upgrades at Gracemar Farms boost efficiency and extend system life.
Alpine engineered a custom dairy chiller retrofit that addressed Gracemar Farms' ammonia challenges while extending equipment lifespan. Instead of replacing the system with another short-lived setup, Alpine designed a solution built for long-term durability and efficiency.
By integrating an advanced clean-room layout and heat recovery system, Alpine captured waste heat that had previously been lost, repurposing it to provide warm water for livestock and boiler preheat. The result: improved air quality, reduced operating costs, and a system designed to last decades instead of years.

Heat recovery tanks at Gracemar Farms capture waste energy to provide warm water for livestock and boiler preheat.
Early results from the Gracemar Farms dairy chiller retrofit show a dramatic improvement in system longevity and efficiency. Equipment that once lasted only ~7 years is now projected to run for 25-30 years, cutting capital replacement costs and ongoing maintenance demands.
The retrofit's integrated heat recovery system also captures energy that was previously wasted, repurposing it to provide warm water for livestock and boiler preheat. This innovation has reduced operating expenses while supporting more sustainable farm operations.
The project further enabled Gracemar Farms to qualify for IAF sustainability grants, underscoring Alpine's role in delivering not just technical solutions but financial and environmental benefits as well.
This retrofit gave Gracemar Farms a cost-efficient, long-term solution that improved reliability, lowered operating costs, and advanced sustainability. The design is serviceable, durable, and sets a new benchmark for agricultural HVAC retrofits across British Columbia.

Custom refrigeration equipment at Gracemar Farms designed for efficiency, durability, and sustainable farm operations.
The Gracemar Farms dairy chiller retrofit proved that agricultural HVAC upgrades can be practical, repeatable, and scalable. By working with existing infrastructure and integrating heat recovery, Alpine created a retrofit model that avoids costly replacements while delivering long-term efficiency.
This retrofit model has already gained attention from other dairy and agricultural operations across BC. Rising energy costs and sustainability requirements mean farms need solutions that balance budget, compliance, and efficiency - and Alpine's approach delivers exactly that.
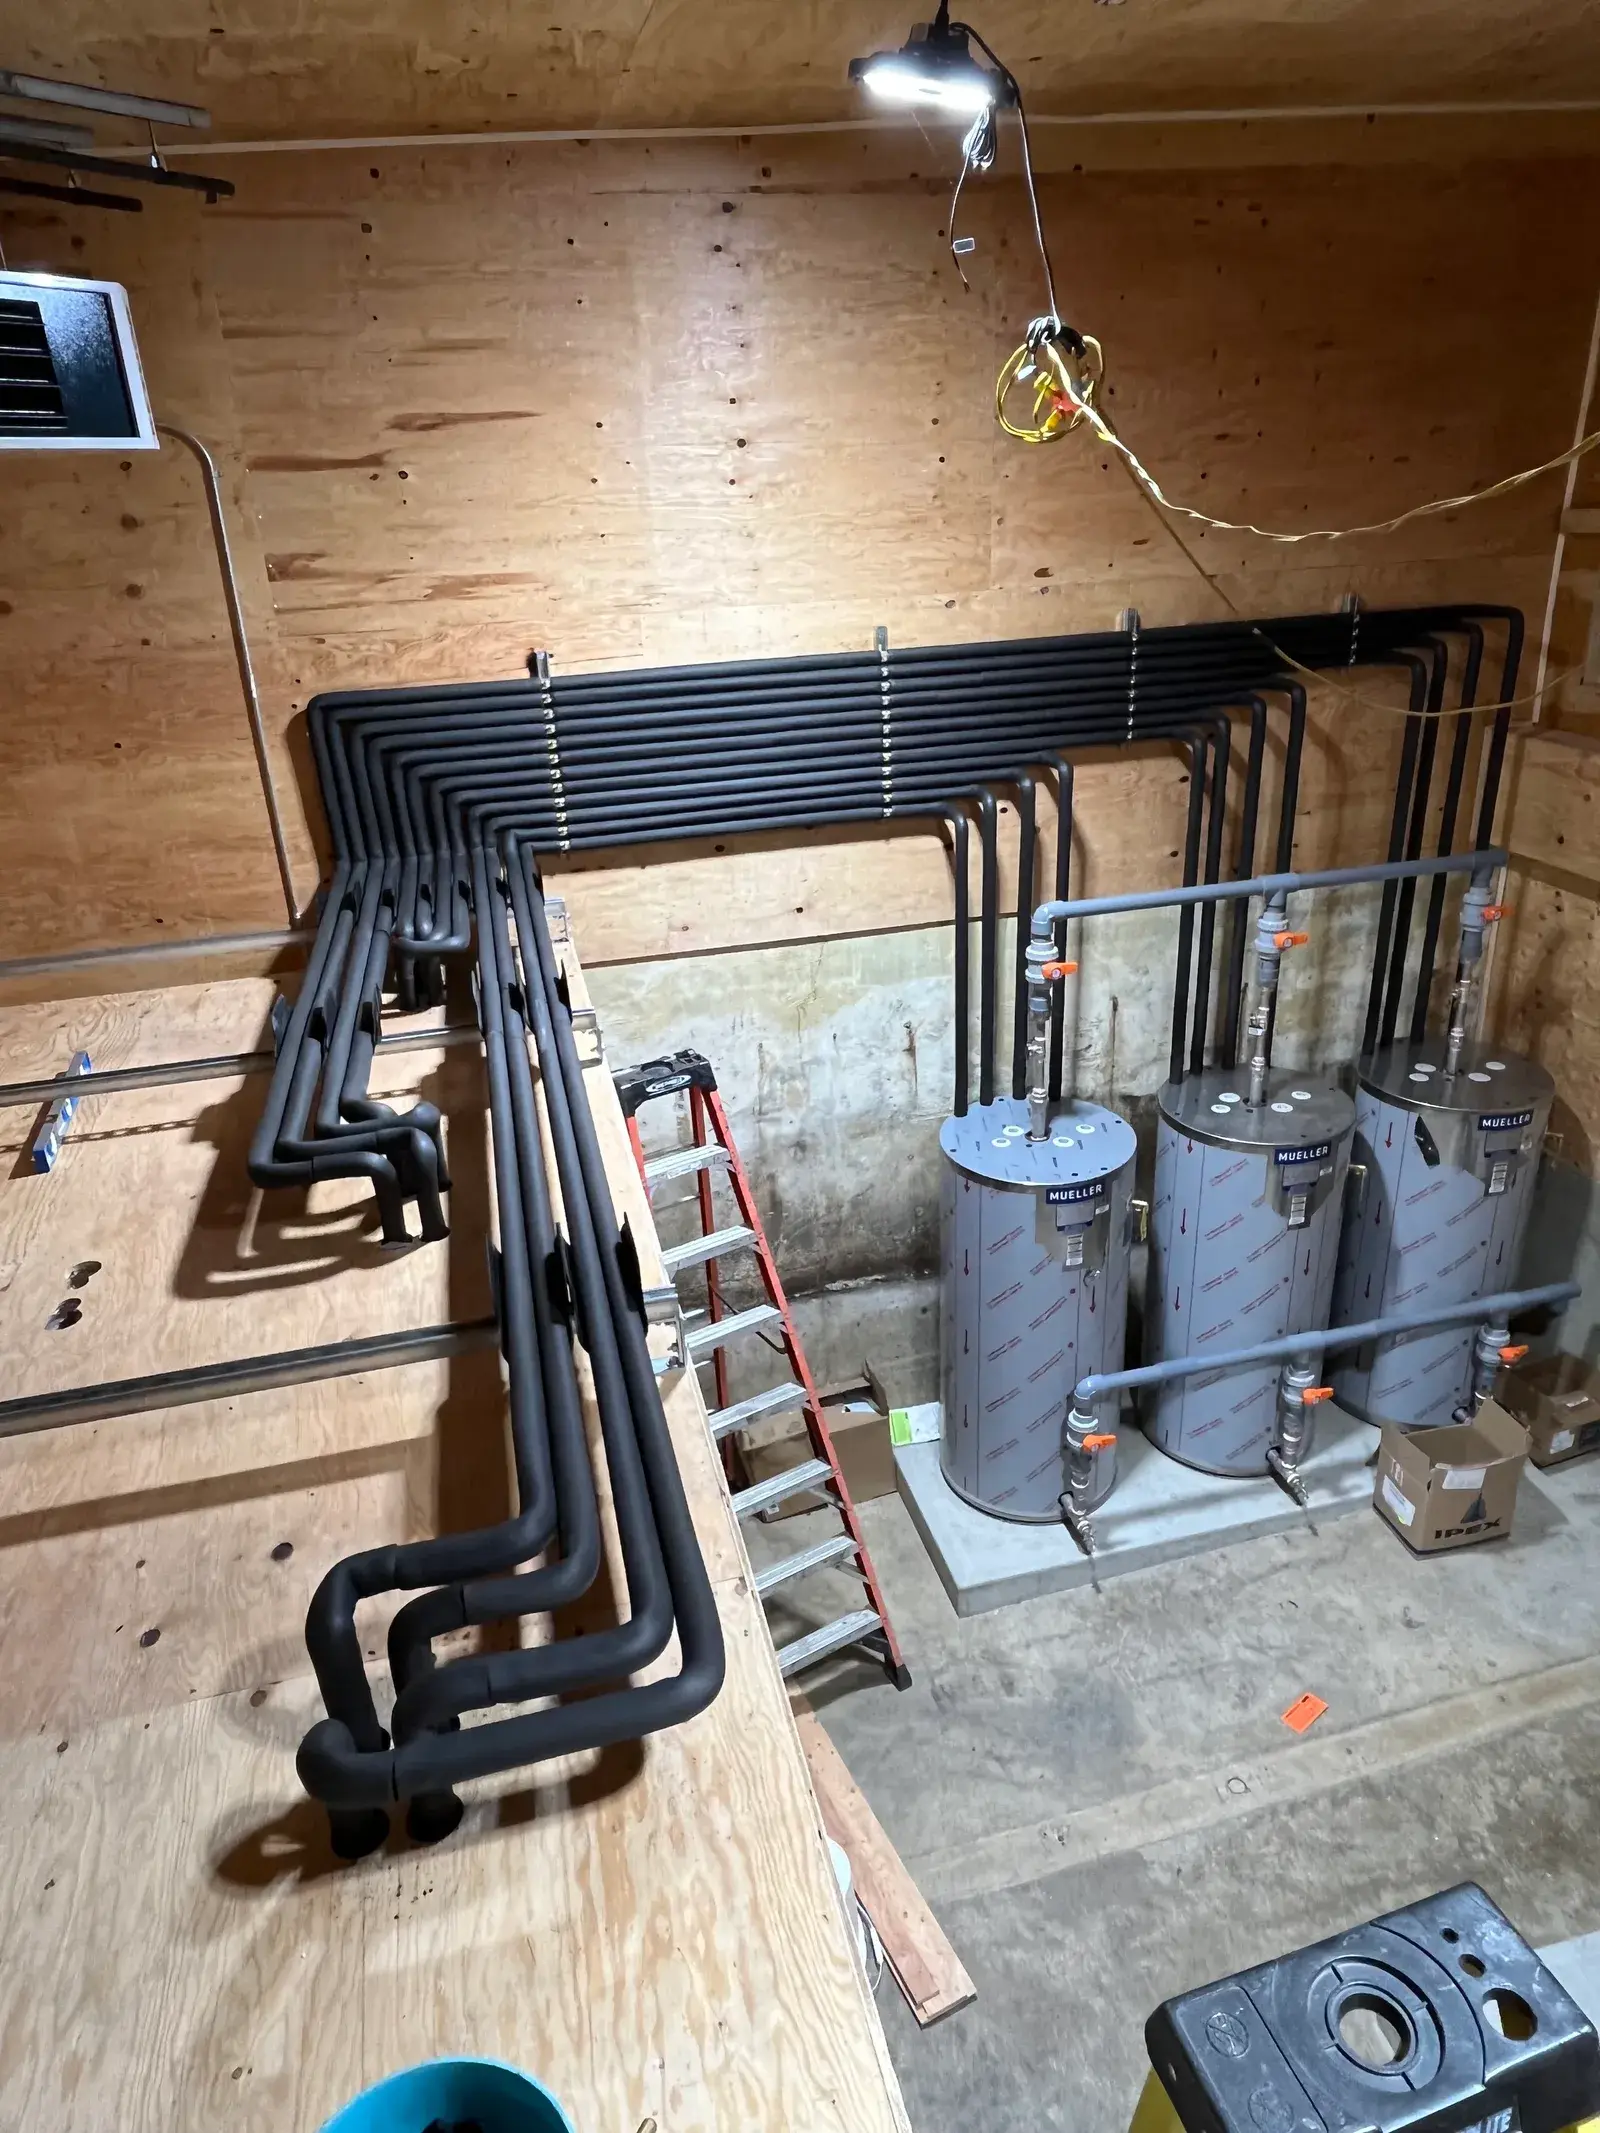
A built-in heat recovery loop captures energy that would normally be lost - heat the refrigeration plant once rejected straight to outside air now preheats water for livestock and cleaning, cutting utility bills every day.
Custom engineering, practical solutions, built farm-tough.
Alpine engineered a custom chiller system specifically for Gracemar Farms, ensuring consistent cooling that keeps up with dairy production and protects valuable equipment.

The system incorporates clean-room style ammonia controls, providing industrial-grade safety standards that protect both workers and equipment.
The system was designed with easy-to-manage controls and a rugged build, ensuring reliable performance and lower maintenance needs for years to come.
Whether you're upgrading outdated chillers, planning a heat recovery retrofit, or working toward sustainability goals, Alpine Refrigeration brings the technical expertise and proven project experience to get the job done right. Contact us today to schedule a site assessment or consultation.
Schedule a Farm Facility Assessment · 604.795.5777